
 Current position > News detail
『Refrigerant Flow Meter for R&D Lab: High-Tier Sensors for Advanced Thermodynamics』Related information(clamp on meter|electromagnetic meter|venturi meterrotameter|orifice meter|ultrasonic flow meter|mass flow meter|coriolis mass flow meter|coriolis flow meter|magnetic flow meter|magmeter flow meter|magflow flow meter|mag meter flow meter|electromagnetic flow meter|vortex flow meter|turbine flow meter|thermal mass flow meter|thermal flow meter|rotameter flow meter)
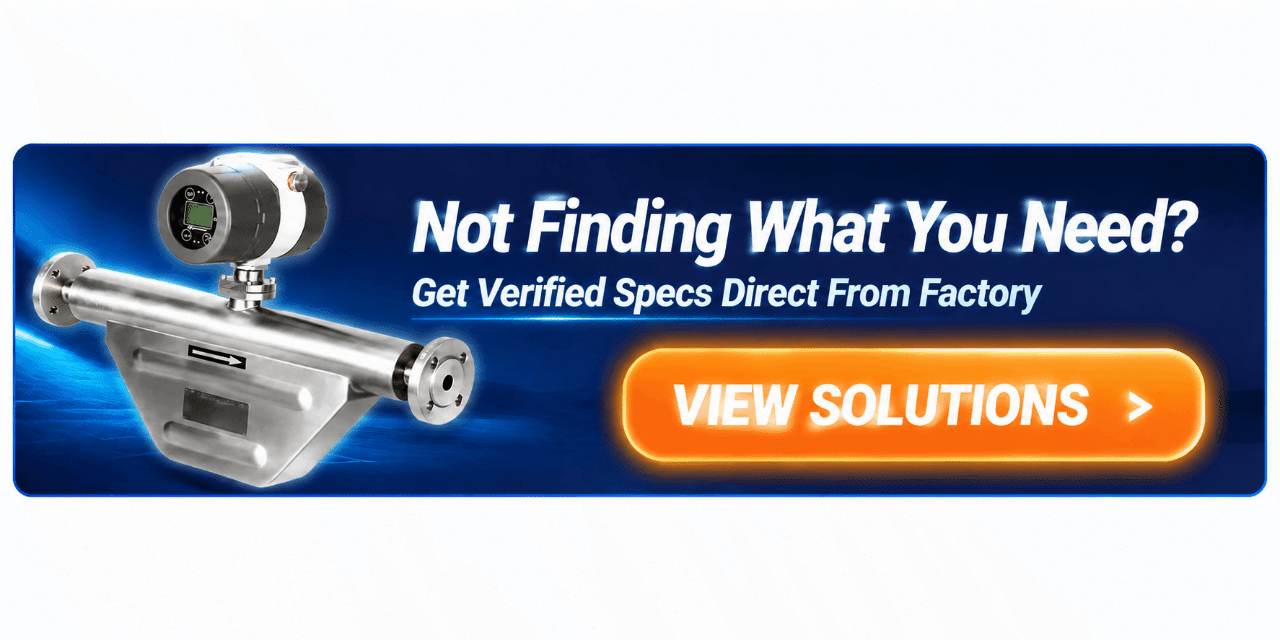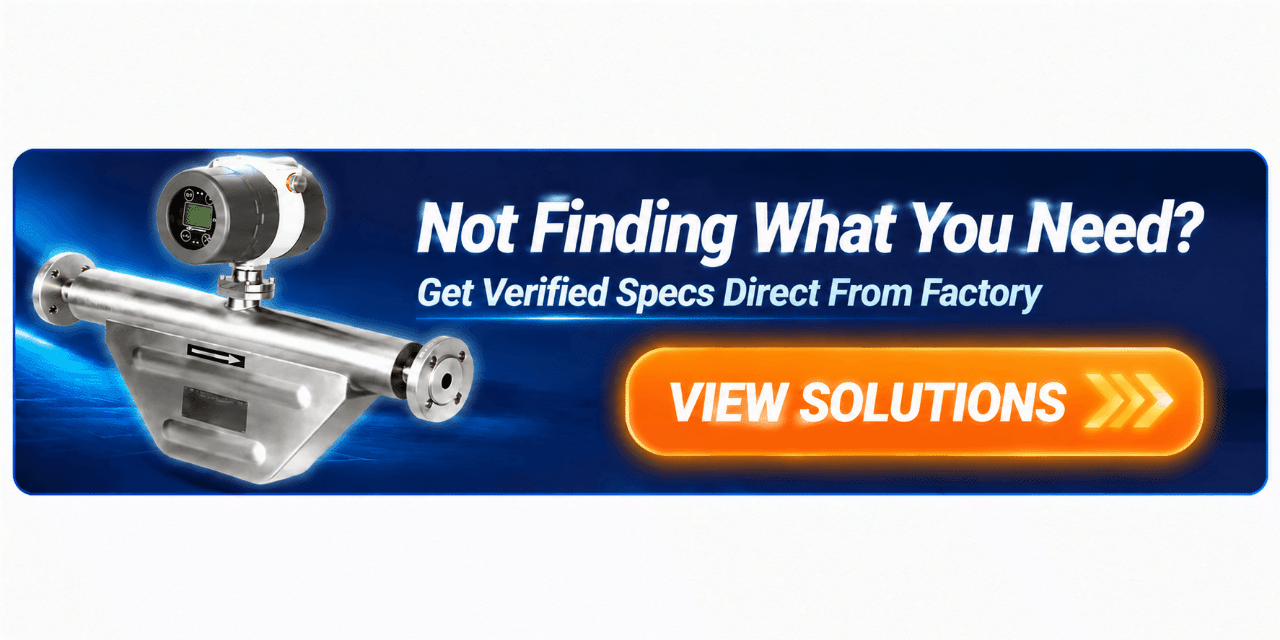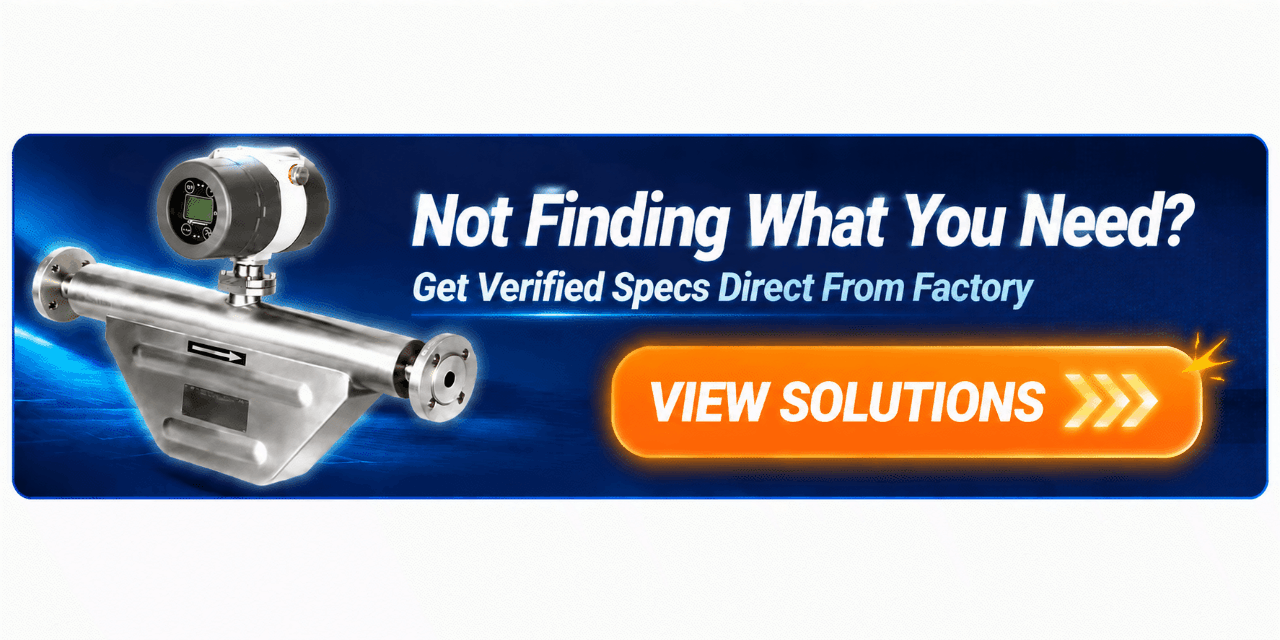
Refrigerant Flow Meter for R&D Lab: High-Tier Sensors for Advanced Thermodynamics
Quick Answer: For refrigerant flow measurement in thermodynamics R&D, a Coriolis mass flow meter from Silver Automation Instruments gives you direct mass flow, density, and temperature data in one device. It handles two-phase refrigerant blends, works from -50 °C to +200 °C, and delivers ±0.1% rate accuracy. No straight pipe runs are needed, so it fits crowded test benches.
Why a General-Purpose Flow Meter Fails in Refrigerant R&D
Lab technicians often grab a turbine or a variable area meter when they start a refrigeration cycle test. Within days they notice drifting readings. Refrigerants like R-32, R-290, or R-1234yf have low viscosity near 0.1 cP in the liquid line. Tiny bearing friction inside a turbine meter introduces repeatability errors above 0.5%. And a glass tube rotameter cannot log data or talk to LabVIEW.
Then there is oil carryover. Even a dry-expansion evaporator lets a small amount of POE oil circulate. The oil forms a liquid film on electrodes inside a magnetic flow meter. Mag meters also fail because most pure refrigerants are non-conductive. Dielectric constants below 2 make electrode-based sensing impossible. So the lab ends up with a maintenance nightmare. We have seen this on customer sites many times. A university lab in Kuala Lumpur replaced three volumetric meters in 14 months before they called us.
Coriolis Meter: The Lab Standard for Refrigerant Mass Flow
A Coriolis flow meter directly measures mass flow, not volume. That matters because refrigerant density changes sharply with temperature and pressure. A 1 °C shift near saturation can swing the density by 2 to 3 percent. Volume-based meters force you to add temperature and pressure compensation, piling up sensor errors. A Coriolis sensor from Silver Instruments eliminates that math. The measurement tube vibrates at its natural frequency. The phase shift between two pick-up coils gives a mass flow signal in kg/h. The resonant frequency itself gives live density in kg/m³. One sensor, three outputs: mass flow, density, temperature.
For an R&D lab testing a heat pump with R-290, the burner test bench typically runs from 2 kg/h up to 60 kg/h. Our DN06 Coriolis meter covers 0–100 kg/h with a turndown of 1:500. The same meter reads 0.1 kg/h during idle circulation. No recalibration, no bypass loop. Because the tube is stainless steel 316L, it withstands ammonia traces during absorption chiller experiments. PTFE liners are not needed. Just specify Hastelloy C-22 wetted parts if your refrigerant blend contains high chloride additives. Most engineers skip this part until they see pitting on a 304 stainless tube after 18 months.
4-20 mA HART, Modbus RTU, and Lab Data Integration
A standalone meter is useless if it cannot stream data to a test rig PLC or a Python script. Our refrigerant flow meters ship with 4-20 mA HART as standard. You get two analog outputs: one for mass flow, one for density. The digital HART signal lets you poll the third variable—temperature—on the same pair of wires. In practice, most labs use the RS-485 Modbus RTU output. A single twisted pair connects the meter to an NI USB-485 interface, and you read all three variables at 50 ms intervals. We tested this setup with a customer in Bandung, Indonesia. They logged 10 data points per second for a month-long compressor durability run without a single CRC error.
For high-speed transient analysis, the meter also provides a pulse output. You can set 1 pulse per 0.1 gram resolution in the configuration menu. A Keysight DAQ captures those pulses during a defrost cycle when flow reverses for 4 seconds. Because a Coriolis meter is bi-directional, it reads negative flow natively. No check valve or manifold rework needed. That alone saved the Bandung lab 12 engineering hours per test campaign.
Operating Limits: Temperature, Pressure, and Two-Phase Flow
Refrigerant labs push the envelope. You might run a transcritical CO₂ test at 130 bar and 120 °C. Our standard sensor body holds up to 200 bar at 20 °C ambient. We derate that to 150 bar at 150 °C process temperature. If your test matrix goes to 180 °C, we can supply a high-temperature version with remote electronics. The drive coil and pick-up coils sit in a separate housing connected by a 3 m armoured cable. This keeps the electronics below 60 °C even when the sensor tube runs hot.
Here is the thing about two-phase refrigerant. A Coriolis meter can handle up to 30% gas volume fraction before the reading becomes noisy. In a direct-expansion evaporator outlet, the vapor fraction might hit 100% for seconds during a step change. For those moments, the meter goes into damping mode. The built-in DSP increases the averaging window automatically. You lose some response speed but the output remains stable. Once the liquid slug returns, damping drops back to 0.2 second. Users can tune the damping threshold via the local display or HART.
ATEX Zone 1 and Lab Safety for Hydrocarbon Refrigerants
R-290 (propane) and R-600a
Last year a customer in Oman built a new calorimeter lab for R-290 chiller development. The local civil defence required Ex-certified instruments on all refrigerant lines. We supplied two DN15 Coriolis meters with ATEX tags and the Oman TRC conformity certificate within 21 days. They commissioned the lab in six weeks instead of the planned ten. The customer told us the quick documentation turnaround was the deciding factor.
Typical Lab Configuration and Dimensions
A refrigerant R&D setup often uses DN06 or DN08 meters in the liquid line and a DN15 meter in the discharge gas line. The DN06 sensor body weighs only 3.2 kg and fits in a 250 mm spool length. Process connections are ¼ inch compression fittings or NPT threaded. Face-to-face dimensions match common Swagelok adapters, so you do not need custom tubing. The meter installs in any orientation. When mounted vertically with upward flow, any residual vapour bubbles rise through the tube and do not accumulate. That eliminates aeration noise in the density reading.
We pre-configure the span and zero before shipping. You tell us your typical flow range, and we set the 20 mA endpoint accordingly. Most R&D labs specify 0–50 kg/h for the liquid line and 0–100 kg/h for the hot gas line. The zero point is calibrated at the factory and stored in the sensor memory. If you later change the transmitter, the new transmitter reads the sensor calibration coefficients automatically. No field re-calibration needed.
Comparing a Coriolis Meter with Other Flow Technologies for Refrigerant
We often get asked about ultrasonic clamp-on meters. They are non-intrusive, which sounds appealing. But clamp-on ultrasonic depends on the pipe wall transmissivity and the fluid sound speed. Refrigerant sound speed varies wildly with temperature and phase. A 5 °C change near the bubble point can cause a 15% measurement error. For any lab needing better than 1% accuracy, clamp-on ultrasonic is not reliable. Vortex meters need a minimum Reynolds number above 20,000 to generate stable vortices. In small-diameter refrigerant liquid lines at low velocity, the Reynolds number often stays below 10,000. The vortex shedding becomes irregular, and the meter under-reads.
Positive-displacement oval gear meters trap a fixed volume per revolution. They work well with hydrocarbon fuels, but refrigerant evaporation inside the gear chambers causes cavitation. That damages the gears over time. We replaced an oval gear meter at a food freezing R&D centre in Chile. The gears had eroded after 8 months with R-744 flash gas. The Coriolis meter sitting in its place has now run 3 years with no wear parts.
Ordering Information: What to Specify
When you send us a request, include the following details so we can propose the right model within 24 hours:
Refrigerant type and oil percentage
Minimum, normal, and maximum flow rate in kg/h
Process temperature range in °C
Maximum operating pressure in bar
Pipe size and connection type (DN, NPT, compression)
Output requirement: 4-20 mA HART, Modbus RTU, pulse
Hazardous area classification if applicable (ATEX, IECEx)
Data acquisition system details (labVIEW, PLC, DCS)
Send these to [email protected] or reach us via WhatsApp: +86-25-52155837. For urgent technical selection, call our engineering team at +86-25-68650347. We offer a fixed-price repair and calibration service for the life of the meter. Our calibration bench is accredited to ISO 17025 for mass flow.
FAQ: Refrigerant Flow Meters for R&D Labs
Q: What accuracy can I expect when measuring R-410A with 3% oil miscibility?
A: The mass flow accuracy remains at ±0.1% of rate. Oil changes the mixture density slightly, but the Coriolis principle measures total mass independently of fluid composition. The density reading will reflect the average density of the refrigerant-oil mixture, usually within ±0.0005 g/cm³.
Q: Can a Coriolis meter measure refrigerant flow during a defrost cycle where flow direction reverses?
A: Yes. The meter is bi-directional by design. The 4-20 mA output can be configured for both directions, with 4 mA at -100% flow, 12 mA at zero, and 20 mA at +100% flow. The pulse output captures reverse flow as a separate count if your DAQ supports quadrature decoding.
Q: Do I need straight pipe runs before and after the meter?
A: No. Coriolis meters are immune to velocity profile distortion. You can install an elbow or a